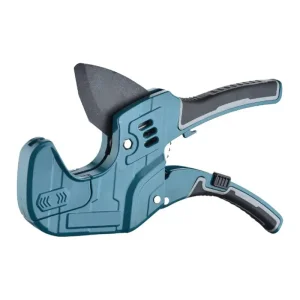
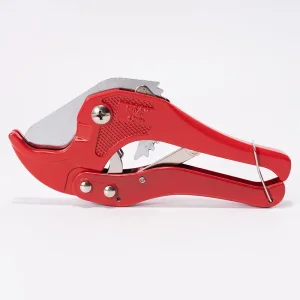
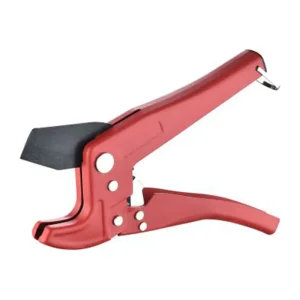
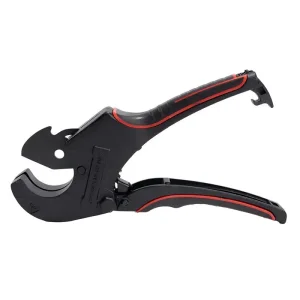
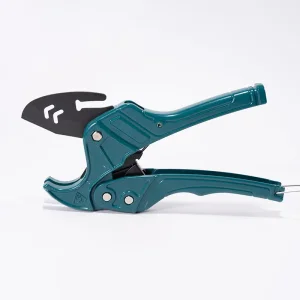
Featured Pipe Preparation & Welding Tools
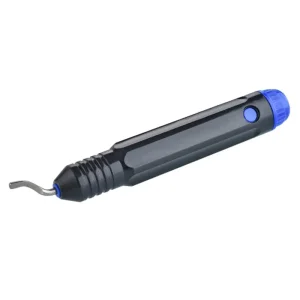
Precision-engineered cutting and deburring equipment designed for heavy-duty operational standards in Kazakhstan's civil and industrial piping projects.
Navigating Kazakhstan's Infrastructure Growth & Industrial Demand
As the economic engine of Central Asia, Kazakhstan is undergoing unprecedented urbanization and industrial expansion. Major municipal development initiatives across key economic hubs such as Almaty, Astana (Nur-Sultan), Shymkent, and Atyrau are driving immense structural demand for reliable, long-lasting thermomechanical piping systems. Polypropylene Random Copolymer (PPR) pipes have emerged as the primary choice for hot and cold water distribution, district heating networks, and aggressive industrial fluid handling.
However, operating in Kazakhstan presents severe environmental and technical challenges. Winter temperatures frequently drop below -30°C to -40°C in northern regions, causing standard plastic materials to freeze and become brittle during installation. Executing leak-free, structurally sound socket fusion welds under these climatic extremes demands high-precision PPR welding equipment featuring precise digital microprocessor control, rapid thermal recovery, and rugged chassis designs.
Furthermore, compliance with local regulatory frameworks, including ST RK (State Standards of the Republic of Kazakhstan) and Eurasian Economic Union (EAEU) technical regulations (TR CU), is mandatory. As an experienced ODM manufacturer, we provide custom PPR welding platforms tailored specifically to meet these stringent regional operational criteria.
Kazakhstan Operational Footprint
- Severe Climate Adaptability: Heating plates optimized with fast-response PID controllers for stable thermofusion at sub-zero ambient temperatures.
- Cross-Border Freight Efficiency: Direct rail and road logistics access via Khorgos Gateway and Alashankou for low-latency supply chains.
- Dual Power Standard Support: Machines calibrated for standard 220V/50Hz grids as well as heavy-duty mobile gas-generator power setups used in remote steppe oilfield sites.
- Local Certification Readiness: Turnkey ODM documentation supporting EAC and ST RK market compliance.
Solving Sourcing Bottlenecks for Global EPC Contractors & Distributors
Overseas procurement managers sourcing plumbing and pipe fusion tools face rising pressures regarding quality assurance, lead time reliability, and total cost of ownership (TCO).
Information Gain & Quality Differentiation
Many low-cost fusion tools suffer from cold spots across socket heating dies, leading to improper polymer cross-linking and catastrophic joint failures under hydraulic pressure tests. Our ODM factories implement dual-element cast aluminum heating plates with matrix heating wire layouts, achieving uniform heat density across all die sizes from 20mm up to 160mm.
Triple-Layer PTFE Coating Standard
Pipe sticking during socket removal damages melted PPR surfaces, introducing air voids into joints. We utilize Japanese Daikin premium non-stick PTFE coating (minimum 50 microns thickness) on all welding sockets. This ensures clean separation, eliminates plastic residue buildup, and extends die lifespan by over 300% under continuous jobsite usage.
Central Asian Logistics Integration
Leveraging direct multimodal logistics corridors connecting Ningbo/Shanghai via Western China to Almaty and Nur-Sultan, we offer bulk buyers stabilized lead times (12-18 days transits). Our export packaging features reinforced metallic carry cases and drop-tested master cartons to survive overland truck transport across mountain terrain.
Technical Roadmap: Next-Gen Thermofusion Systems
Continuous technological iterations driving precision, safety, and energy efficiency for professional plumbing crews.
Phase 1: Microprocessor-Driven Smart Temperature Control (PID)
Transitioning from traditional mechanical thermostat switches to intelligent digital microcontrollers. Maintains target fusion temperature (typically 260°C ± 2°C) automatically compensating for ambient thermal drag in extreme environments like northern Kazakhstan winters.
Phase 2: Off-Grid Cordless & Gas-Powered Fusion Solutions
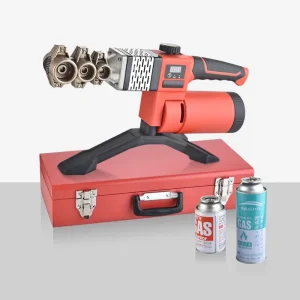
Pioneering fuel-efficient 1.4KW gas-powered portable socket fusion tools. Eliminates reliance on bulky electrical generators or extension cables when installing pipelines in unpowered agricultural, mining, or rural construction sites across Central Asia.
Phase 3: AI-Assisted Joint Integrity Verification & Data Logging
Integrating Bluetooth IoT module options into premium ODM lines. Contractors can track heating cycles, soak times, and temperature curves on mobile devices to provide digital QA verification reports for municipal infrastructure authorities.
Standard Socket Fusion Welding Parameters
To ensure structural compliance with DVS 2207-11 standards, our PPR welding tools are calibrated to precise heating, changeover, and cooling profiles:
| Pipe Outer Diameter (mm) | Heating Depth (mm) | Heating Time at 20°C (sec) | Cold Climate Heating Time (-5°C) (sec) | Max Changeover Time (sec) | Cooling Time (min) |
|---|---|---|---|---|---|
| 20 mm | 14.0 mm | 5 sec | 8 sec | 4 sec | 2 min |
| 25 mm | 15.0 mm | 7 sec | 11 sec | 4 sec | 2 min |
| 32 mm | 16.5 mm | 8 sec | 12 sec | 6 sec | 4 min |
| 40 mm | 18.0 mm | 12 sec | 18 sec | 6 sec | 4 min |
| 50 mm | 20.0 mm | 18 sec | 27 sec | 6 sec | 4 min |
| 63 mm | 24.0 mm | 24 sec | 36 sec | 8 sec | 6 min |
* Note: Operating in ambient conditions below 0°C requires a 50% increase in heating duration. Our ODM machines feature customized pre-heat boost modes to streamline this process.
Full ODM Customization Ecosystem
We empower importers, regional distributors, and tool brand owners serving Central Asia with complete private-label engineering:
- Customized housing color schemes matching your corporate identity (RAL/Pantone).
- Laser-engraved brand logos on aluminum heating plates and die sockets.
- Bilingual instruction manuals (Russian/Kazakh/English) ensuring jobsite safety compliance.
- Custom steel carrying cases with high-density EVA foam cutouts for accessories.
ISO9001 & Quality Control Protocols
Every welding unit leaving our facility undergoes rigorous multi-stage quality verification to guarantee zero field failures:
- Die-Electric Strength Testing: High-voltage breakdown insulation checks up to 1500V.
- Thermal Stability Audit: 48-hour continuous power burn-in testing to verify thermostat accuracy.
- Drop & Impact Resistance: Structural casing strain tests mimicking real-world construction site handling.
- Defect Tracking: Full serial number traceability backed by a 1-year factory warranty replacement guarantee.
Frequently Asked Questions (FAQ)
Clear insights regarding technical specifications, ODM customization, and logistics for Kazakhstan procurement.
Explore Our Full Pipeline Tool Catalog
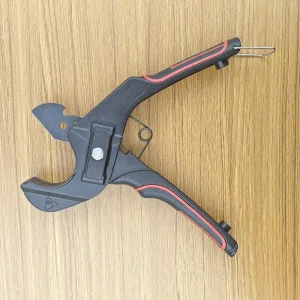
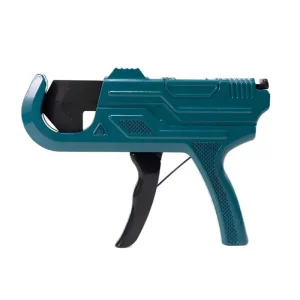
Complete your procurement matrix with our professional-grade cutters, calibrators, and specialized fusion machines.
Ready to Elevate Your PPR Fusion Tool Line in Kazakhstan?
Get direct access to factory pricing, custom engineering drawings, and sample evaluation packages within 24 hours.
Send Inquiry Now