Featured Pipe Cutting & Preparation Equipment
Explore our core series of high-precision manual ratchet cutters, heavy-duty aluminum shears, and calibration tools essential for preparing flawless PPR, PVC, PEX, and HDPE piping joints before socket thermo-fusion.
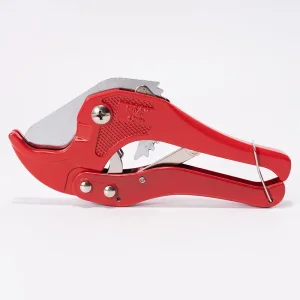
OEM Heavy-Duty 42mm Aluminum Pipe Cutter from China Suppliers - Professional Quality PVC Cutting Tool
Request Wholesale Quote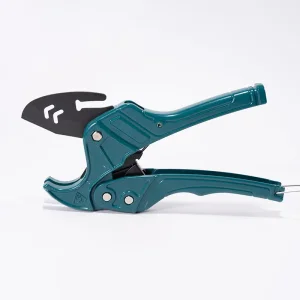
Wholesale 42mm Ratchet Plastic PPR Pipe Cutter - Model 42922 by China Suppliers and Factory for PVC, PPR, PEX Pipes
Request Wholesale Quote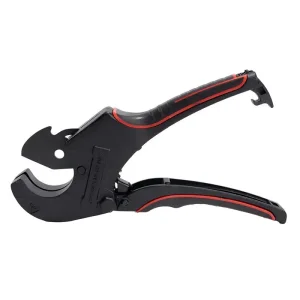
OEM High-Efficiency 42mm Ratchet PVC Pipe Cutter - Leading China Suppliers & Factory for Rapid Construction
Request Wholesale Quote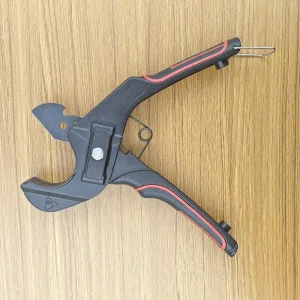
ODM China Suppliers: 36mm Precision PEX Pipe Cutter from Factory - Eliminate Installation Failures in Tight Spaces
Request Wholesale Quote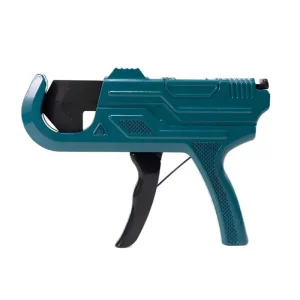
China 42mm Compact Ratchet Pipe Cutter for Narrow Spaces – Reliable Performance by China Suppliers and Factory
Request Wholesale Quote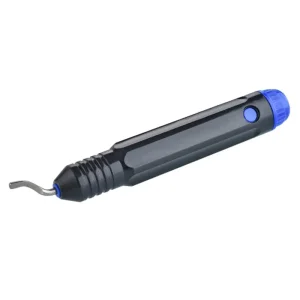
China M2 HSS Deburring Tool DT-001 for Metal & Plastic Pipes - Quality China Suppliers & Factory Manufacturers
Request Wholesale Quote
Wholesale Heavy-Duty Adjustable PVC Pipe Cutter from China Suppliers - Model JC-PC-22 for Professional Use
Request Wholesale Quote
OEM China HDPE Pipe Cutter Suppliers - Professional 63mm One-Handed Tools from a Trusted Factory Supplier
Request Wholesale QuoteThe Engineering Evolution of PPR Socket Fusion Technology
A comprehensive study on thermal molecular bonding, micro-processor PID temperature stabilization, and supply chain scalability for global plumbing tool procurement managers.
Molecular Homogenous Fusion Mechanism
Polypropylene Random Copolymer (PPR-80 and PPR-100) requires precise thermal activation within the tight temperature window of 260°C ± 5°C. Modern high-volume infrastructure projects demand thermo-fusion tools capable of maintaining absolute thermal equilibrium across heating matrices. When molten PPR reaches its exact melt flow index (MFI), socket and pipe end surfaces intertwine at the molecular level, creating a unified, seamless joint that exhibits structural strength equal to or exceeding the original pipe wall. Our manufacturing facility engineers aluminum heating plates with embedded high-density dual heating elements to prevent localized cold zones during rapid jobsite welding cycles.
Eliminating Joint Failure via DVS 2207 Standards
In accordance with German DVS 2207-11 guidelines for hot element socket welding of thermoplastic pipes, heating times, changeover intervals, and cooling cycles must be strictly controlled. Inferior PPR heating welding machines suffer from thermal inertia, causing material degradation (overheating above 270°C leading to inner diameter constriction) or cold welds (underheating below 255°C resulting in catastrophic pressure leaks). By integrating advanced microprocessor-driven PID temperature controllers and high-grade Japanese Daikin PTFE matrix-coated die sockets, our factory guarantees zero-sticking performance, ultra-fast heat transfer, and superior tensile endurance across 50-year system lifespans.
Why Global Importers Partner with Our China PPR Welder Factory
Located in Yuyao, Zhejiang — the heartland of world-class hardware tooling and polymer technology — our state-of-the-art facility delivers uncompromised OEM manufacturing advantages.
Die-Cast Aluminum Metallurgy
We utilize ADC12 high-grade aluminum alloys for die-casting heating plates. This provides optimal thermal conductivity, warp resistance under high pressure, and maximum structural integrity during extended industrial usage on job sites.
Triple-Layer Japanese PTFE Coating
Every socket die (from 20mm to 160mm) undergoes automated sandblasting followed by triple-layer spray coating with Japanese-imported PTFE fluoropolymer. This guarantees 3,000+ fusion cycles without plastic adhesion or surface stripping.
Dual-Switch Heat Boost Circuitry
Our professional thermo-fusion machines feature dual independent heating elements (e.g., 800W + 700W = 1500W total output). Installers can operate single circuits for smaller pipes or activate both switches for rapid heating of thick-walled industrial pipes.
Strict ISO9001 Quality Control
From incoming raw material spectrographic analysis to 100% 2-hour electrical insulation resistance and temperature calibration testing before packaging, every machine adheres to stringent ISO9001 and CE quality standards.
Custom OEM/ODM Branding Solutions
We provide full-spectrum OEM services, including custom iron box colors, laser-engraved brand logos, bespoke handle molds, voltage customization (110V/220V/240V), and regional plug configurations (EU, UK, US, AU).
Breakthrough Gas-Powered Innovation
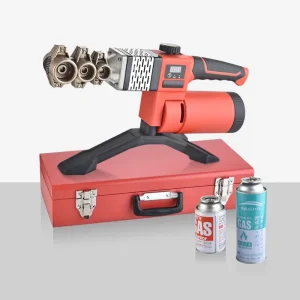
Addressing the major industry pain point of off-grid plumbing installations, our factory designed the world-leading SGS/CE-certified Gas-Powered PPR Fusion Welder—enabling cordless operation anywhere without generators.
Standard Socket Fusion Parameters & Heating Guidelines
Refer to our factory engineering benchmark table for PPR pipe socket fusion welding cycles (compliant with DVS 2207-11 standards).
| Pipe Outer Dia. (mm) | Wall Thickness (SDR Spec) | Heating Time at 260°C (sec) | Changeover Time Max (sec) | Cooling Time Total (min) | Recommended Machine Power (W) |
|---|---|---|---|---|---|
| 20 mm | 2.0 - 3.4 mm (SDR 6 / 7.4) | 5 sec | 4 sec | 2 min | 800W - 1000W |
| 25 mm | 2.3 - 4.2 mm (SDR 6 / 7.4) | 7 sec | 4 sec | 2 min | 800W - 1000W |
| 32 mm | 2.9 - 5.4 mm (SDR 6 / 7.4) | 8 sec | 6 sec | 4 min | 800W - 1500W |
| 40 mm | 3.7 - 6.7 mm (SDR 6 / 7.4) | 12 sec | 6 sec | 4 min | 1500W - 2000W |
| 50 mm | 4.6 - 8.3 mm (SDR 6 / 7.4) | 18 sec | 6 sec | 5 min | 1500W - 2000W |
| 63 mm | 5.8 - 10.5 mm (SDR 6 / 7.4) | 24 sec | 8 sec | 6 min | 1500W - 2000W |
| 75 - 110 mm | 6.8 - 18.3 mm (Heavy Commercial) | 30 - 50 sec | 8 - 10 sec | 8 - 10 min | 2000W - 2500W Benchtop |
Macro-Industry Engineering Solutions
Our thermo-fusion welding machines and prep tools are deployed worldwide across complex residential, commercial, industrial, and agricultural piping projects.
High-Rise Residential Potable Water Systems
Potable hot and cold water networks require hygienic, non-toxic joints. PPR thermo-fusion eliminates the need for chemical solvents, solder flux, or mechanical threaded connections, ensuring zero risk of heavy metal leaching or joint loosening over structural lifespans.
HVAC Hydronic & Radiant Floor Heating
Underfloor heating loops and central hydronic heating risers experience continuous thermal expansion and contraction cycles. Homogeneous PPR socket fusion creates permanent leak-proof joints capable of withstanding operating pressures up to PN25 at elevated temperatures.
Chemical Processing & Industrial Fluid Transport
PPR pipes possess outstanding chemical resistance against aggressive acids, alkalis, and industrial fluids. Our high-precision welding machines ensure smooth internal weld beads that prevent media buildup, turbulence, or localized chemical stress cracking.
Remote Municipal & Off-Grid Infrastructure
In rural water supply projects or new construction sites lacking grid electricity, our innovative 1.4KW Gas-Powered PPR Fusion Welder allows field engineers to perform continuous socket welds using standard butane/LPG cartridge canisters without heavy gasoline generators.
Shipbuilding & Maritime Water Networks
Marine environments demand non-corrosive piping systems. PPR socket fusion welding produces vibration-resistant, lightweight, salt-water-proof pipeline connections ideal for commercial vessels, offshore platforms, and aquaculture facilities.
Commercial Hardware Retail & Private Label Distribution
We supply international tool brands, regional hardware distributors, and big-box home improvement chains with turn-key private-label OEM packages, including retail color boxes, blister packaging, custom manual translation, and localized safety certifications.
Global Enterprise Procurement & Quality Assurance Standard
How we help procurement officers, brand managers, and wholesale importers reduce total cost of ownership (TCO) while guaranteeing absolute zero-defect delivery.
1. High-Volume Direct Factory Pricing
By eliminating intermediary trading agents and operating directly out of our 2,667 m² Yuyao manufacturing facility equipped with over 40 automated CNC processing stations, we provide global buyers with unbeatable factory-direct pricing scales for container-load orders (FOB, CIF, DDP terms available).
2. Rapid OEM Customization & Sampling
Speed-to-market is critical. We provide 3D CAD modeling, custom color matching (RAL/Pantone codes), and physical prototype sample delivery within 7 working days. OEM branding customization includes laser marking, customized molded carrying cases, and private-label instruction manuals.
3. Zero-Risk International Compliance
All PPR heating welding machines, pipe cutters, deburring tools, and calibrators are fully certified to international standards. We provide complete CE declaration of conformity, ISO9001 documentation, SGS safety audit reports, and RoHS material compliance certificates required for smooth customs clearing in North America, Europe, South America, and the Middle East.
4. Flexible Logistics & Inventory Support
Located in close proximity to Ningbo and Shanghai Ports, our factory handles sea freight, air freight, and multimodal logistics efficiently. We support mixed-model container consolidation, allowing distributors to order pipe cutters, deburring tools, calibrators, and PPR welders in a single shipment.
Frequently Asked Questions (FAQ)
Expert engineering answers to common technical, procurement, and application questions regarding wholesale PPR heating welding machines.
What is the optimum operating temperature for PPR pipe socket welding?
The standard fusion temperature for Polypropylene Random Copolymer (PPR) pipes is strictly 260°C (500°F) ± 5°C. Heating below 255°C results in insufficient polymer melting and weak joint strength, while heating above 275°C causes material degradation, excess bead formation, and internal pipe constriction. Our welding machines feature digital thermostat sensors and PID control modules to maintain precise temperature stability.
How does a Gas-Powered PPR Fusion Welder compare to standard electric models?
Gas-powered PPR welders utilize compact gas cartridges (butane/LPG) to generate rapid heating without requiring electrical outlets or heavy fuel generators. They are ideal for remote job sites, outdoor agricultural pipelines, emergency repairs, and high-elevation work. Electric models (800W–2000W) are preferred for continuous indoor commercial plumbing where grid power is readily available.
Why is Teflon (PTFE) coating quality so crucial for socket die heads?
During socket thermo-fusion, molten PPR plastic contacts the surface of the heating sockets. If the coating is thin or low quality, molten plastic will stick to the die, burning during subsequent cycles and creating structural defects in the weld. We apply triple-layer Japanese Daikin PTFE coating to our die heads, ensuring zero adhesion, easy wipe-cleaning, and extended service life over thousands of cycles.
What is the minimum order quantity (MOQ) for OEM private label manufacturing?
Our standard MOQ for OEM private label requests (custom steel case colors, laser-engraved logos, custom outer cartons) starts at 500 units per model. For standard stock models with factory packaging, flexible smaller order quantities are supported to assist distributors with initial market testing.
Why is pipe deburring and calibration necessary before PPR heating welding?
When cutting plastic or multilayer PEX-AL-PEX/PPR pipes, uneven edges, burrs, or oval deformation frequently occur. Using high-precision pipe deburring tools and calibrators restores absolute roundness and creates a clean chamfered edge. This ensures smooth insertion into the heated socket die without scraping off molten polymer, preventing premature joint leaks.
Additional Plumbing & Fusion Tool Systems
Browse our complete catalog of specialized pipe deburrers, heavy-duty copper tube cutters, adjustable plastic pipe shears, and gas-powered fusion welders direct from our factory lines.
OEM M2 HSS Deburring Tool for Metal & Plastic Pipes - DT-001 from China Suppliers & Factory
Request Wholesale Quote
Wholesale Heavy-Duty 1.25-inch Copper Tube Cutter | China Suppliers & Factory for Professional Plumbing Tools
Request Wholesale Quote
ODM Heavy-Duty Adjustable PVC Pipe Cutter 63mm – High-Performance China Suppliers & Factory Model JC-PC-22
Request Wholesale Quote
China Heavy-Duty Adjustable PVC Pipe Cutter for Professionals - China Suppliers and Factory Model JC-PC-22
Request Wholesale Quote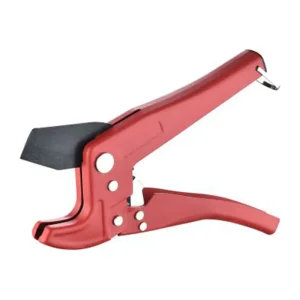
Wholesale 42mm Heavy-Duty Ratchet Plastic Pipe Cutter Model PC-25 - China Suppliers Tool for PPR, PVC, PE Pipes
Request Wholesale Quote
OEM M2 HSS Deburring Tool DT-001 for Metal & Plastic Pipes - China Factory Suppliers for Professional Finishing
Request Wholesale Quote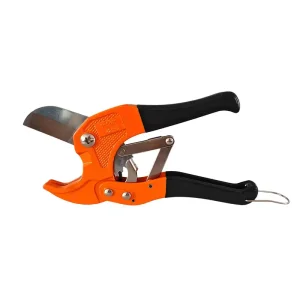
OEM Professional 42mm PVC Pipe Cutter with Anti-Slip Dipping Handle - China Suppliers and Factory Quality Tool
Request Wholesale Quote