Featured PPR Fusion & Pipe Tooling Systems
Factory-direct OEM/ODM manufacturing engineered to strict DIN 16962 and EN ISO 15874 international standards.
1. Executive Summary & Global PPR Procurement Dynamics
Polypropylene Random Copolymer (PPR) piping systems represent the foundational infrastructure for contemporary potable water distribution, industrial fluid transport, and HVAC hydronic networks. As global construction sectors transition toward sustainable, zero-corrosion fluid transport, demand for precision-engineered PPR socket fusion welding machinery has expanded at an unmatched trajectory. Securing a certified OEM PPR Welding Manufacturer is no longer merely a procurement transaction; it is a strategic imperative to ensure structural joint integrity, eliminate catastrophic joint failure risks, and optimize total cost of ownership (TCO).
Industrial thermal fusion relies on homogenous molecular bonding. Unlike mechanical crimping or chemical solvent welding, socket heat fusion melts the external wall of the PPR pipe and the internal matrix of the socket fitting simultaneously at specified thermal thresholds (typically 260°C ± 5°C). When joined under governed pressure, the polymer chains intermingle, forming a single, continuous pressure-rated structure. OEM manufacturing parameters must strictly govern heating plate flatness, thermal distribution uniformity, and PTFE coating durability to guarantee homogeneous fusion joints across varied global environmental conditions.
Macro Market Drivers & Regional Demand Patterns
Analysis of procurement data reveals distinct regional requirements across major industrial markets:
- European Union & UK: Heavy emphasis on digital PID microprocessors with real-time temperature logging, compliance with DVS 2207-1 parameters, and low-energy dual-stage heating elements.
- Middle East & GCC Region: Demand for high-wattage thermal output (up to 2000W) capable of maintaining 260°C in high ambient temperature variations, alongside rugged die-cast aluminum chassis.
- Latin America & Southeast Asia: High volume requirements for versatile 20mm-63mm portable socket fusion kits with rapid-heating capabilities and high-abrasion resistance carrying cases.
- North America: Accelerated adoption of PPR-RCT (Polypropylene Random Crystallinity Temperature modified) tools requiring refined pressure-holding duration metrics.
2. Engineering & Manufacturing Technological Roadmap
Advanced metallurgical selection, thermodynamic modeling, and algorithmic thermal regulation in OEM PPR welder production.
Microprocessor Temperature Regulation
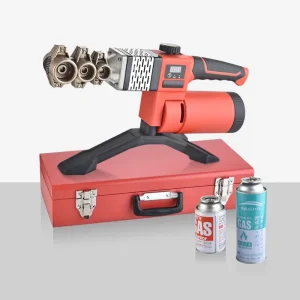
Integration of solid-state relays (SSR) and PID fuzzy logic controls maintains a precise temperature matrix of 260°C ± 2°C, preventing polymer degradation caused by thermal spikes or cold-weld failures caused by heat drops.
Multi-Layer PTFE Die Matrices
Socket dies are cast from high-density aluminum alloy and coated with triple-layer Japanese Daikin PTFE. This guarantees non-stick polymer release, eliminates resin drag, and withstands over 3,000 thermal cycles.
Cordless & Gas-Powered Innovation
Pioneering off-grid 1.4KW gas-powered combustion technology for job sites lacking electrical supply, achieving rapid warm-up times under 3 minutes with total portability.
OEM Production Benchmarks & Technical Specifications
| Performance Indicator | Standard Professional Grade | Industrial Heavy-Duty Line | Gas-Powered Off-Grid Line |
|---|---|---|---|
| Pipe OD Capacity Range | 20mm – 63mm (1/2" - 2") | 20mm – 160mm (1/2" - 6") | 20mm – 32mm (1/2" - 1-1/4") |
| Rated Power Output | 800W – 1000W Dual Element | 1500W – 2000W High Capacity | 1.4KW Equivalent Thermal Output |
| Temperature Tolerance | ± 3°C (Thermostatic Analog) | ± 1°C (Digital PID Controller) | ± 4°C (Internal Gas Governor) |
| Die Matrix Coating | Double-Layer PTFE | Triple-Layer Daikin Heavy-Duty PTFE | Specialized High-Temp Non-Stick PTFE |
| Insulation Resistance | > 1 MΩ | > 5 MΩ (Reinforced Dielectric) | Non-Electrical Combustion Circuit |
| Compliance Certifications | CE, LVD, EMC, ISO9001 | CE, SGS, ISO9001, DVS 2207-1 | CE, SGS Gas Directive Certified |
3. B2B Customization Framework & OEM Production Lifecycle
From engineering CAD blueprints to turnkey branded retail blow-molded cases, our manufacturing line integrates complete white-label flexibility.
4. Quality Control Protocols & Global Regulatory Standards
Structural integrity in thermal pipe welding leaves no room for error. A single cold joint or overheated polymer seam in a commercial high-rise building can result in multi-million dollar water damage claims. As a certified OEM PPR welding manufacturer, our facility executes multi-stage inspection routines engineered to surpass standard commercial metrics.
1. Tensile Shear Testing
Welded pipe samples undergo destructive tensile pull testing to ensure the joint withstands higher stress than the pipe body itself.
2. Hydrostatic Pressure
Fused connections undergo continuous 95°C pressure testing at 16 bar for over 1,000 consecutive hours under DIN 8077 guidelines.
3. Microscopic Cross-Section
Micro-section analysis inspects fusion boundaries for voids, pinhole air pockets, or material oxidation.
4. Electrical Safety Verification
100% of manufactured units undergo hi-pot insulation voltage testing, earth grounding continuity checks, and leakage testing.
DVS 2207-1 Standard Heat Fusion Parameters Overview
Proper machine calibration must enable operators to execute the exact heating, changeover, and cooling time intervals specified by DVS 2207-1 rules:
| Pipe Outer Diameter (OD) | Heating Depth (mm) | Heating Time at 260°C (sec) | Max Changeover Time (sec) | Cooling Time Total (min) |
|---|---|---|---|---|
| 20 mm | 14.0 mm | 5 sec | 4 sec | 2 min |
| 25 mm | 15.0 mm | 7 sec | 4 sec | 2 min |
| 32 mm | 16.5 mm | 8 sec | 6 sec | 4 min |
| 40 mm | 18.0 mm | 12 sec | 6 sec | 4 min |
| 50 mm | 20.0 mm | 18 sec | 6 sec | 5 min |
| 63 mm | 24.0 mm | 24 sec | 8 sec | 6 min |
5. Industrial & Commercial Application Environments
Our specialized PPR socket fusion machinery and pipe preparation tools are deployed across diverse global infrastructure projects.
Municipal Hot & Cold Water Networks
Primary distribution lines in high-density residential developments require leak-free continuous fusion joints capable of withstanding constant 10-bar working pressure and thermal expansion cycles.
Industrial Chemical Fluid Transport
PPR's high resistance to aggressive acids and alkalis makes it ideal for chemical processing facilities. Our precise thermal tools ensure uniform wall thickness at fusion joints to eliminate localized stress corrosion.
HVAC Chilled Water & Radiant Heating
Hydronic cooling and floor heating systems demand high-volume socket joining. Our rapid-heating dual-element fusion plates speed up joint completion by 35% on large construction sites.
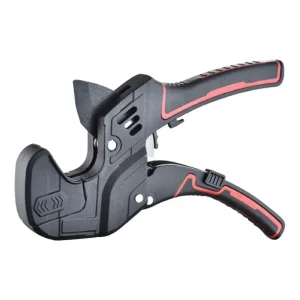
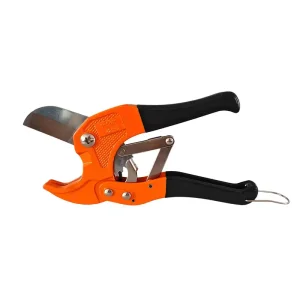
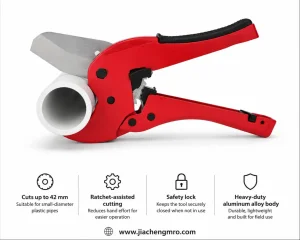
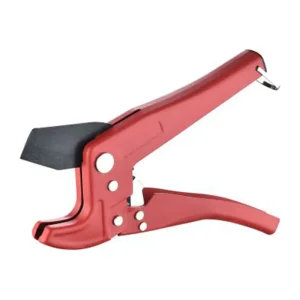
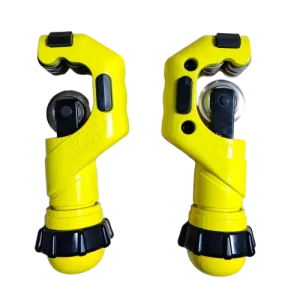
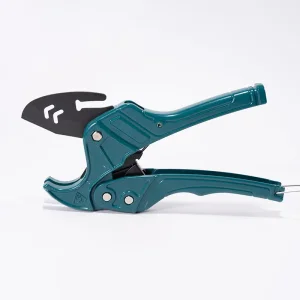
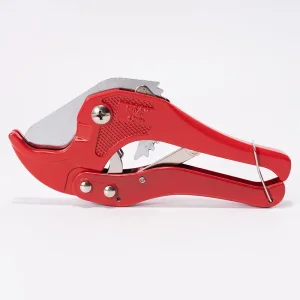
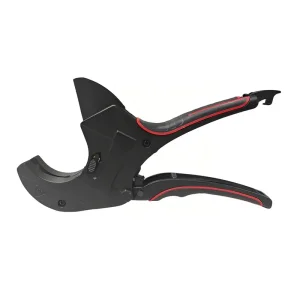
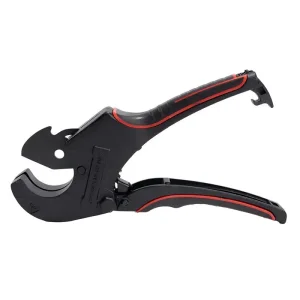
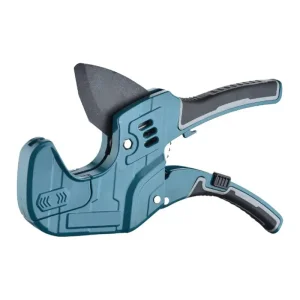
Complete Pipe Preparation & Cutting Product Line
Complementary professional pipe cutters, deburring systems, and specialized fusion accessories.
6. Frequently Asked B2B Procurement Questions (FAQ)
Detailed technical and commercial guidance for wholesale distributors, tool brand owners, and OEM buyers.
Partner with a Premier OEM PPR Welding Manufacturer
Expand your product catalog with high-yield thermal fusion welders, precision pipe cutters, and deburring systems backed by ISO9001 and CE certifications. Contact our B2B engineering team today for factory pricing and custom tool samples.