Featured Thermoplastic Welding & Precision Tools
Factory-direct engineered socket fusion machinery, gas-powered cordless welders, and specialized pipe preparation cutters.
Comprehensive Guide to ODM Socket Fusion Welder Manufacturing & Global Supply Chain Optimization
In modern civil infrastructure, municipal water distribution, industrial chemical transport, and residential HVAC systems, polyolefin piping networks (PPR, PE, PE-RT, and PB) have largely superseded traditional metallic conduits. The operational integrity of these piping networks relies overwhelmingly on the molecular cohesion achieved during thermal joining processes. Socket fusion welding—a process wherein matching male heating bushings and female heating sockets melt the exterior pipe surface and interior fitting socket simultaneously—remains the gold standard for leak-free, permanent polyolefin pipe connections.
As a premier ODM (Original Design Manufacturer) and OEM Socket Fusion Welder Factory operating out of Yuyao, Zhejiang Province—China's global epicenter for hardware and plumbing tool manufacturing—we engineered this whitepaper to provide global procurement executives, technical directors, and OEM tool distributors with deep, authoritative insights into socket fusion technology, manufacturing economics, thermal metallurgy, and customized global procurement strategies.
1. Polymer Thermodynamics & The Physics of Socket Fusion
Achieving a homogenous, high-strength socket fusion joint requires strict adherence to polymer-specific thermomechanical windows. Thermoplastic materials such as Polypropylene Random Copolymer (PPR-Type 3) do not transition instantaneously from a solid state to a liquid state; rather, they undergo a viscoelastic transformation past their crystalline melting temperature ($T_m \approx 160^\circ\text{C}$).
For effective socket fusion, the welding heating element must deliver a sustained operational temperature of 260°C (500°F) across the heating matrix. If the heating element drops below 245°C, cold fusion occurs, creating cold lap defects, mechanical weakness, and micro-voids that fail pressure tests under hydrostatic shear stress. Conversely, if localized temperatures exceed 275°C, thermal degradation (pyrolysis) breaks down the polymer's long-chain hydrocarbon backbone, causing material charring, reduced pressure rating, and premature joint failure under thermal cycling.
Thermostatic Heating Control
Our ODM welders incorporate dual-stage digital PID microcontrollers or high-precision mechanical thermostats capable of maintaining set temperatures within a tight tolerance band of ±2°C under fluctuating jobsite voltages.
DuPont PTFE Socket Coating
Die-cast sockets feature multi-layer Japanese or DuPont-grade PTFE (Teflon) fluoropolymer non-stick coatings, preventing polymer adhesion, burning, and residue buildup over thousands of heating cycles.
Die-Cast Heating Plates
Formed from high-purity ADC12 aluminum alloy with embedded high-watt-density stainless steel tubular heating elements, delivering rapid thermal recovery within 3 minutes from a cold start.
2. Sourcing Advantages of China's Socket Fusion Manufacturing Ecosystem
Sourcing ODM socket fusion machinery and complementary pipe cutters from qualified China factories provides global brands with undeniable economic and engineering scaling capabilities. The Yuyao/Ningbo hardware cluster in Zhejiang represents the world's most densely integrated manufacturing hub for pipe installation tools.
- Complete Vertical Integration: Raw aluminum ingots, stainless steel heating tubes, copper internal wiring, precision CNC machining, PTFE electrostatic spray coating, and electronic circuit assembly are executed within a 15-kilometer supply chain radius. This localized ecosystem minimizes lead times and insulates production schedules from global logistics disruptions.
- Extreme OEM/ODM Customization Flexibility: China manufacturers excel at custom tooling development. Whether your catalog requires customized voltage options (110V US standard, 230V EU Europlug, 240V UK 3-pin), specialized wattage outputs (600W, 800W, 1500W, 2000W), ergonomic handle molds, brand-matched colors (Pantone matching), or customized blow-molded carrying cases, factories can rapidly produce prototype tooling within 15–20 business days.
- Strict Compliance & International Certification: Modern Chinese manufacturing facilities operate under ISO9001:2015 Quality Management Systems. Products destined for European and North American professional supply channels undergo rigorous testing to obtain GS, CE, EMC, LVD, and RoHS compliance certificates.
Technical Engineering Comparison Matrix
Benchmarking Thermoplastic Pipe Joining Technologies & Structural Equipment Specifications
| Fusion / Joining Method | Applicable Pipe Range | Primary Thermoplastic Polymeric Materials | Heating Temperature & Control | Joint Strength & Pressure Rating | Optimal Field Application Scenario |
|---|---|---|---|---|---|
| Socket Fusion Welding | DN 20mm – DN 125mm (1/2" to 4") | PPR, PE, PE-RT, PB | 260°C ± 2°C (Digital PID / Thermostatic) | Homogeneous Molecular Bond (> PN25 rating) | Indoor plumbing, hydronic HVAC, residential hot/cold water, tight riser spaces. |
| Gas-Powered Socket Fusion | DN 20mm – DN 32mm | PPR, PP-H, PE | 1.4KW Gas Burner System (Cordless) | High Cohesion (Matches standard electrical welder) | Off-grid jobsites, remote infrastructure, utility repairs where electricity is unavailable. |
| Butt Fusion Welding | DN 63mm – DN 1200mm+ | HDPE, PE100, PP-B | 200°C – 220°C (Hydraulic / Manual Pressure) | End-to-End Axial Weld (Equal to original pipe strength) | Long-distance municipal water mains, gas pipelines, heavy industrial discharge lines. |
| Electrofussion Welding | DN 20mm – DN 630mm | HDPE, PE100, PE-Gas | Barometric / Smart Barcode Voltage Control | Embedded Resistance Wire Fusion (Ultra-High Integrity) | Gas supply lines, hazardous chemical conduits, underground high-pressure mains. |
| Multilayer Calibration & Pressing | DN 16mm – DN 32mm | PEX-AL-PEX, PERT-AL-PERT | Mechanical Compression / O-Ring Sealing | Mechanical Joint (PN16 - PN20) | Radiant floor heating distribution, gas manifold connections, flexible interior plumbing. |
Industry Trends & Macro-Level OEM Solutions
Next-generation technological shifts shaping global plumbing tool procurement and field performance standards.
1. Cordless & Gas-Powered Autonomy
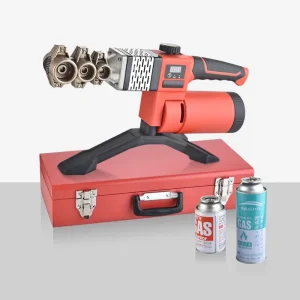
Traditional socket fusion welders rely heavily on uninterrupted 220V/110V power mains or heavy diesel generators. The industry is rapidly adopting cordless gas-powered fusion welders (e.g., 1.4KW LPG/Butane units) and high-capacity lithium-battery powered heating platforms. These solutions eliminate cord hazards and drastically reduce setup time for utility crews working in remote or newly constructed buildings.
2. Digital Microprocessor Control & Data Logging
Modern commercial specifications require verifiability. Advanced ODM welders are integrating smart LED/LCD displays driven by 32-bit ARM microprocessors. These modules track heating time, cooling time, ambient air temperature compensation, and joint countdown timers, ensuring plumbers execute textbook fusion cycles compliant with DVS 2207-1 standards.
3. Zero-Burr Precision Cutting Integration
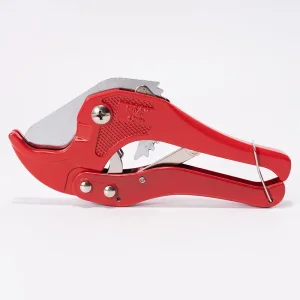
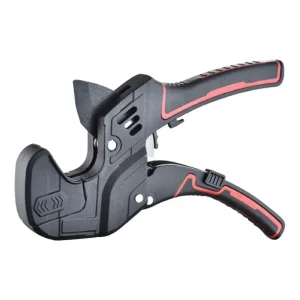
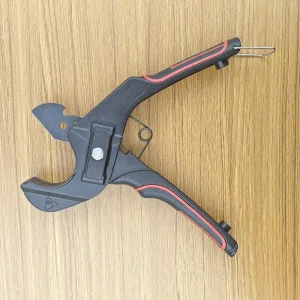
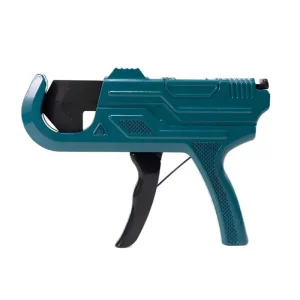
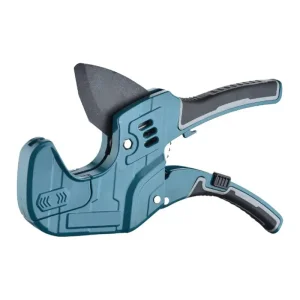
Socket fusion fails if pipe ends are cut elliptically or with extensive burrs that score the interior non-stick socket. Top-tier ODM suppliers bundle their fusion machines with industrial 42mm, 50mm, or 63mm ratchet pipe cutters featuring SK5 or 8Cr13MoV high-carbon stainless steel blades, ensuring clean, perpendicular cuts every time.
Localized Application Scenarios & Field Engineering
Tailored operational setups for diverse global markets and plumbing infrastructure conditions.
Residential PPR Plumbing Rework
Challenge: Working inside narrow drywall cavities or cramped under-sink basements where standard heavy welders cannot maneuver.
Solution: Compact 800W socket fusion units featuring slimline heating plates and dual-mounting socket positions (front tip socket attachment) combined with 36mm narrow-space PEX/PPR cutters.
Off-Grid Municipal & Agricultural Lines
Challenge: Installing agricultural irrigation lines or remote rural water supply networks across open terrain without portable electrical generators.
Solution: Cordless 1.4KW Gas-Powered PPR Fusion Welders operating on standard butane cartridges, allowing plumbers to move freely along kilometers of trenching without dragging power extension cables.
Industrial Chemical & High-Pressure HVAC
Challenge: Joining thick-walled SDR6 PPR or High-Density Polyethylene (HDPE) pipes up to 110mm requiring zero wall deformation and deep heat penetration.
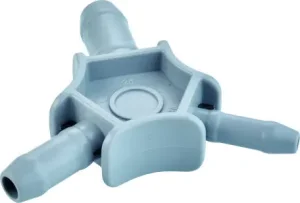
Solution: High-power 1500W-2000W dual-element welders equipped with heavy-duty floor stands, floor clamps, and calibrated 3-in-1 pipe calibrators to round out pipe ends before socket insertion.
Frequently Asked Questions (OEM Sourcing & Engineering FAQ)
Clear, definitive technical and commercial answers for global procurement professionals.
Q1: What is the optimal heating time schedule for socket fusion of PPR pipes?
Heating time varies strictly by outer diameter (OD) and wall thickness under standard DVS 2207-1 guidelines. At a set temperature of 260°C: a 20mm PPR pipe requires 5 seconds heating, 4 seconds insertion time, and 2 minutes cooling; a 32mm pipe requires 8 seconds heating, 6 seconds insertion, and 4 minutes cooling; while a 63mm pipe demands 24 seconds heating, 8 seconds insertion, and 6 minutes cooling. Overheating causes pipe wall collapse and interior flow restriction.
Q2: What is the difference between OEM and ODM services for Socket Fusion Welders?
OEM (Original Equipment Manufacturing) involves manufacturing our existing factory-tested welder models under your private brand label, custom handle color scheme, and packaging. ODM (Original Design Manufacturing) involves full custom engineering—where our factory designs brand-new housing molds, custom electronic PCB controls, specific wattage configurations, and proprietary socket die shapes based on your technical drawing specifications.
Q3: Why is DuPont Teflon coating thickness critical on fusion heating sockets?
During fusion, molten PPR sticks aggressively to bare aluminum. Low-quality socket coatings peel off quickly, causing molten plastic to cling, smoke, and drag material out of the joint, creating major leak paths. We apply a minimum 25-micron double-layer DuPont PTFE fluoropolymer coating that withstands over 3,000 continuous thermal cycles without degradation or loss of non-stick capability.
Q4: How does a gas-powered PPR fusion welder maintain stable temperatures without electrical feedback?
Our gas-powered 1.4KW fusion welders utilize a specially engineered catalytic burner chamber paired with an integrated heat-pipe spreader. The burner delivers a steady BTU output that naturally balances thermal dissipation through the high-density aluminum heat plate, holding equilibrium at 260°C under ambient field operations without needing complex electric sensors.
Q5: What minimum order quantities (MOQs) apply for private label ODM orders?
Standard private-label OEM packaging orders generally start at an MOQ of 500 to 1,000 sets per model (which includes custom color boxes, silk-screened logos, and customized metal toolboxes). For full ODM projects requiring custom die-cast tooling molds, MOQ requirements are evaluated on a project basis alongside NRE (Non-Recurring Engineering) mold agreements.
Q6: How do pipe calibrators prevent joint failures in multilayer PEX-AL-PEX installations?
When multilayer pipe is cut with a standard cutter, the aluminum core deforms into an oval shape, and the inner PE lining develops interior burrs. A 3-in-1 calibrator simultaneously rounds out the pipe end, re-establishes exact internal concentricity, and creates an inner 15-degree chamfer. This prevents the sharp aluminum edge from slicing the internal rubber O-rings of press or compression fittings during insertion.
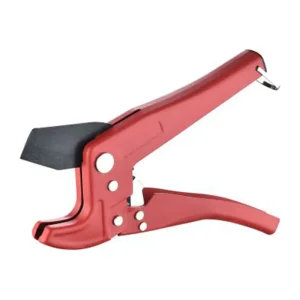
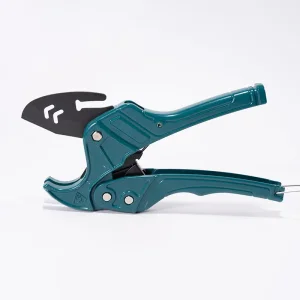
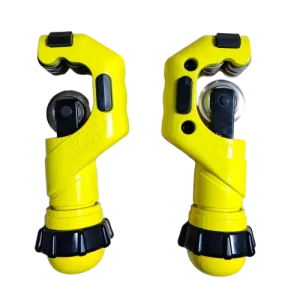
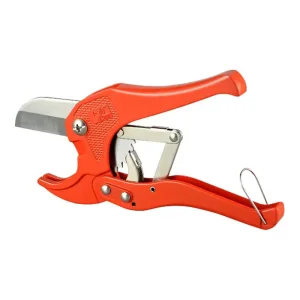
Complete Pipe Installation & Cutter Series
Heavy-duty ratchet cutters, precision aluminum tools, and copper tube cutting machinery direct from China factories.
Partner with a Trusted OEM/ODM Socket Fusion Machinery Specialist
Whether you are expanding your plumbing tool catalog, establishing private-label brand production, or seeking reliable factory direct supply with ISO9001 quality assurance, our Yuyao engineering team is ready to support your market growth.
Request OEM Quotation & Technical Catalog