Engineered for high-stress municipal, residential, and industrial pipe joining operations. Factory-direct wholesale models available for global distributors.
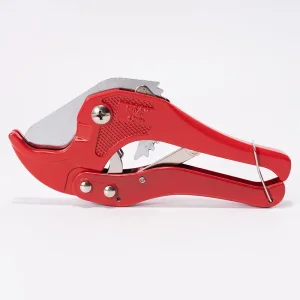
OEM Heavy-Duty 42mm Aluminum Pipe Cutter from China Suppliers
View Specifications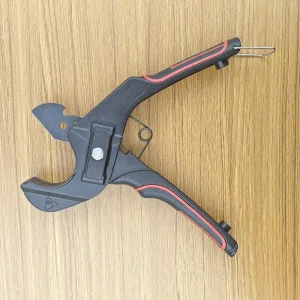
ODM China Suppliers: 36mm Precision PEX Pipe Cutter
View Specifications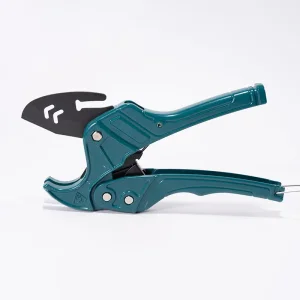
Wholesale 42mm Ratchet Plastic Pipe Cutter - Model 42922
View Specifications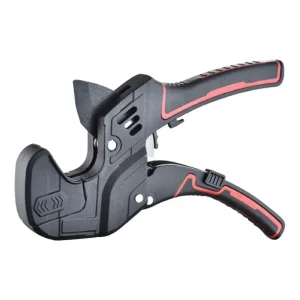
Wholesale Heavy-Duty Adjustable PVC Pipe Cutter - Model JC-PC-22
View Specifications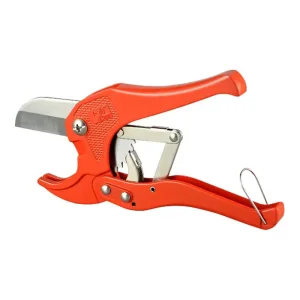
ODM 42mm Manual Plastic Pipe Cutter Model JC-PC-001
View Specifications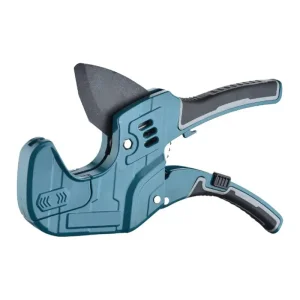
ODM Heavy-Duty Adjustable PVC Pipe Cutter 63mm
View Specifications
China M2 HSS Deburring Tool DT-001 for Metal & Plastic Pipes
View Specifications
OEM M2 HSS Deburring Tool DT-001 for Professional Finishing
View Specifications1. Executive Engineering Summary: Industrial Pipe Welding Architecture
Modern piping infrastructure demands non-destructive, zero-leak integrity across challenging environmental parameters. As a premier China Pipe Welding System Supplier & Factory, our manufacturing framework addresses the precise mechanical, thermal, and chemical dynamics required for joining high-density polyolefins, random copolymer polypropylene (PPR), cross-linked polyethylene (PEX), and polyvinyl chloride (PVC) piping networks.
The industrial pipe welding ecosystem integrates three distinct operational stages: mechanical edge preparation, controlled thermal melting, and stabilization cooling under dwell pressure. Below is a structured categorization of our advanced systems:
Socket & Field Fusion Welders
Utilizing high-purity Teflon-coated heating sockets and gas-powered micro-combustion heat engines, our socket fusion welders operate seamlessly in grid-less remote environments. Designed for PPR, PE, and PB lines ranging from 20mm to 63mm.
Precision Cutting & Calibrators
High-leverage ratchet pipe cutters equipped with Japanese SK5 or M2 High-Speed Steel (HSS) blades guarantee zero-burr, perpendicular cuts. Integrated 3-in-1 calibrators restore circularity in PEX-AL-PEX multilayer pipes prior to press or fusion jointing.
Automated QA & Field Deburring
Rotary edge deburring tools and internal chamfering systems eliminate stress-concentration risers. Designed to prevent inner lumen constriction and safeguard elastomeric O-rings during fitting insertion.
2. Thermodynamics of Thermoplastic Fusion & Mechanical Edge Geometry
Understanding the thermodynamics of plastic pipe fusion is paramount for procurement engineers evaluating factory output. Socket fusion welding does not simply melt plastic; it induces a viscoelastic state where polymer chains untangle and recrystallize across the interface under controlled mechanical pressure.
| Pipe Material | Outer Diameter (mm) | Optimal Heat Temp (°C) | Heating Phase (Sec) | Changeover Max (Sec) | Cooling Time (Min) |
|---|---|---|---|---|---|
| PPR (Polypropylene Random) | 20mm – 32mm | 260 ± 5 | 5 – 8 | 4 | 2 |
| PPR (Polypropylene Random) | 40mm – 63mm | 260 ± 5 | 12 – 24 | 6 | 4 |
| HDPE (PE100 Grade) | 32mm – 63mm | 210 ± 5 | 10 – 18 | 5 | 3 |
| PEX-AL-PEX (Multilayer) | 16mm – 32mm | Calibrated Cold Join / Mechanical Press | N/A | N/A | Instant |
The Mechanical Physics of Blade Cutting & Deburring
A poorly cut pipe creates uneven contact points against the heating socket, resulting in localized hot spots and material degradation (oxidation). Our factory utilizes high-carbon Japanese SK5 alloy steel and M2 high-speed steel treated through vacuum oil-quenching processes. This achieves a blade Rockwell Hardness of HRC 60–63, ensuring sharp force vectoring without wall crushing or radial deformation.
V-Shaped Wedge Geometry
Distributes cutting force symmetrically, preventing structural ovality in thin-walled PVC and PEX pipes during manual or ratchet shearing operations.
Ratchet Step Multipliers
Multiplies mechanical advantage by up to 12:1, allowing field technicians to execute one-handed cuts through 63mm heavy-walled HDPE pipes.
Precision Internal Chamfering
Rotary M2 HSS deburring blades create a smooth 15-degree lead-in chamfer, reducing fitting insertion force by 45% and eliminating stress concentrations.
3. Macro-Industry Turnkey Solutions
Different industrial sectors require distinct jointing methodologies. As a fully integrated China factory, we engineer targeted tooling packages aligned with major global standards (DIN, ASTM, ISO, BS).
Municipal Water Infrastructure
Large-diameter PE100 distribution lines require consistent fusion beads to prevent biological accumulation. Our heavy-duty 63mm HDPE cutters paired with calibrated socket welders prevent inner wall collapse, guaranteeing uninterrupted laminar flow in municipal drinking water networks.
- Zero-contamination Teflon heating sockets
- Full compliance with ISO 4427 standards
- Heavy-duty ratcheting mechanism
HVAC & District Heating
High-temperature PPR-CT and PEX-AL-PEX composite pipes in hydronic heating systems demand precision end calibration. Our 3-in-1 calibrators combine deburring, rounding, and sizing to guarantee zero leakage in press fitting connections under 10-bar continuous thermal stress.
- Simultaneous 16/20/25/26mm sizing capabilities
- Ergonomic aluminum body structure
- Compatible with European press fitting norms
Off-Grid Field Construction
Remote mining camps, agricultural irrigation, and field plumbing often lack access to diesel generators or grid power. Our patented 1.4KW Gas-Powered PPR Fusion Welder delivers instant, flameless heat powered by standard butane gas canisters, eliminating heavy generator transport.
- SGS and CE safety certified
- Rapid 3-minute pre-heat time
- Constant-temperature gas flow regulator
4. China Factory 4.0: Supply Chain Resilience & Quality Yield
Our 2,667 m² manufacturing campus in Yuyao, Zhejiang, leverages advanced automation, ERP-tracked raw material pipelines, and rigorous continuous improvement protocols to set the industry standard for pipe welding and cutting equipment.
100% In-House CNC Machining
We do not rely on third-party machine shops. All cutter handles, gear ratchets, and welder heating plates are precision-milled using multi-axis CNC centers, ensuring tolerance accuracy within ±0.015mm.
Raw Material Quality Control
Every batch of ADC12 aluminum alloy ingot and SK5 high-carbon tool steel undergoes X-ray fluorescence (XRF) spectrographic analysis to verify element composition before entering production lines.
Automated Stress Testing
Every ratchet mechanism undergoes 5,000 continuous cycle load tests under simulated field resistance. Gas welders undergo 72-hour continuous pressure leakage tests prior to final assembly packaging.
5. Enterprise OEM/ODM Global Procurement Process
We streamline private-label tool creation for international tool brands, hardware distributors, and engineering contractors through an end-to-end customized manufacturing protocol.
Engineering & CAD
Submission of technical requirements, custom handle ergonomic modeling, and material selection (Aluminum vs. Die-Cast Steel).
Rapid Prototyping
3D metal printing and CNC prototype creation. Initial sample delivered via express air freight within 10 business days.
Tooling & Mold Setup
Hardened steel mold production for injection handles and aluminum bodies. Automated laser engraving of buyer logos and branding.
Mass Run & Logistics
Full batch run with ISO9001 sampling. Customized retail blister packs, double corrugated export master cartons, and FOB/CIF shipping.
6. Technology Roadmap & Next-Generation Outlook (2026–2030)
As pipe manufacturing transitions to high-performance polymers (such as PE-RT Type II and PEX-a), welding systems must evolve to deliver higher intelligence and lower carbon footprints.
AI Thermal profiling
Integration of infrared micro-sensors on socket fusion plates to dynamically adjust thermal power based on ambient jobsite temperature and wind chill factors, preventing cold-weld failures.
Ultra-Light Alloys
Transitioning traditional aluminum alloy cutter frames to magnesium-lithium and carbon-fiber hybrid structures, reducing overall tool weight by 35% without sacrificing torsional rigidity.
Smart Data-Logging Welders
Development of Bluetooth-enabled field welders that automatically store weld cycle duration, heating plate temperature, and GPS coordinates for automated compliance audit reporting.
7. Global Regulatory Compliance & Regional Standards
Importers must guarantee that tools entering local jurisdictions satisfy regional safety and operational mandates. Our products carry full certification dossiers for seamless customs clearance and retail distribution.
| Target Market | Applicable Certification Standard | Tool Compliance Focus | Documentation Provided |
|---|---|---|---|
| European Union (EU) | CE Directive / EN ISO 12100 / SGS | Gas safety, electrical thermal protection, ergonomic hand force limits | Full CE Declaration of Conformity, SGS Test Reports |
| North America (USA/Canada) | ASTM F1055 / ASTM F2620 / OSHA Compliant | Blade steel hardness specs, pipe beveling dimensions, structural crush resistance | Material Test Certificates (MTC), Hardness Verification |
| Global / Enterprise | ISO 9001:2015 Management System | Complete manufacturing batch traceability, incoming material XRF audit logs | ISO Audit Certificates, Factory Inspection Reports |
8. Frequently Asked Questions (Procurement & Technical FAQ)
Comprehensive engineering and commercial responses to common inquiries from international buyers and distributors.
Q1: What prevents pipe ovality when using manual or ratchet cutters on thin-walled PVC/PEX?
Radial crushing or ovality occurs when blade pressure is concentrated at a single point before cutting shear initiates. Our cutters feature precision V-shaped, double-bevel ground SK5 blades paired with a curved anvil support cradle. This geometry cradles the pipe circumference, ensuring force vectors act radially outward while the razor edge slices through the wall, maintaining 100% cross-sectional roundness.
Q2: How does your gas-powered PPR welding system maintain constant heat without electricity?
Our 1.4KW Gas-Powered PPR Fusion Welder utilizes an integrated micro-combustion chamber equipped with a internal gas-flow governor valve. This valve automatically regulates butane flow despite fluctuating ambient temperatures, maintaining the heating plate temperature within the optimal PPR socket fusion band of 260°C ± 5°C. It is fully certified by SGS and CE for safe field operation.
Q3: Why is post-cut deburring and calibration mandatory for PEX-AL-PEX multilayer pipe installations?
When multilayer pipe is cut, the internal aluminum layer can burr inwardly, while the overall profile slightly flattens. Inserting a press fitting into an uncalibrated pipe can nick or dislodge the elastomeric O-rings, leading to immediate or delayed leaks under thermal cycling. Our 3-in-1 calibrator restores true circularity, bevels the inner plastic sleeve, and creates a clean seat for the sealing rings.
Q4: What is your standard Minimum Order Quantity (MOQ) and production lead time for OEM orders?
For standard catalog items with custom laser branding, our MOQ is 500 units per model. For complete custom injection color molding and private blister packaging, the baseline MOQ is typically 1,000 to 2,000 units. Standard production lead times are 25 to 30 calendar days from sample sign-off and deposit receipt.
Q5: How does your factory handle quality guarantee and defective item replacement?
Every shipment includes a 1-year commercial factory warranty. Because our automated QC process maintains a overall batch defect rate below 0.3%, any manufacturing defect verified via photo/video inspection is instantly compensated with 1:1 replacement stock added to your subsequent sea container order, backed by zero-friction administrative support.
Explore additional factory-direct models engineered for high durability, ergonomic comfort, and precision operation on demanding job sites.
ODM Heavy-Duty 42mm Aluminum PVC Pipe Cutter
View Specifications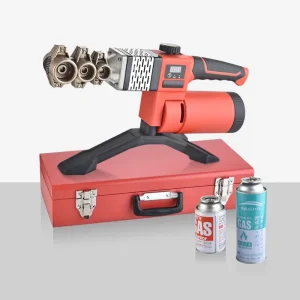
ODM 1.4KW Gas Powered PPR Fusion Welder for 20-32mm Pipes
View Specifications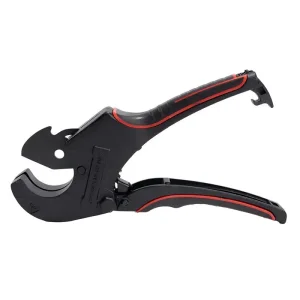
OEM High-Efficiency 42mm Ratchet PVC Pipe Cutter
View Specifications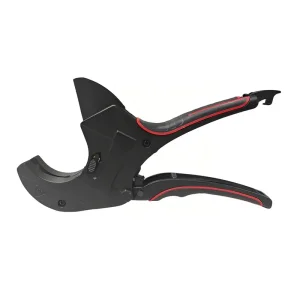
OEM China HDPE Pipe Cutter Suppliers - Professional 63mm Tool
View Specifications
China Heavy-Duty Adjustable PVC Pipe Cutter - Model JC-PC-22
View Specifications
ODM China's Professional 36mm Precision PEX Pipe Cutter
View Specifications
Factory Direct: 1.4KW Gas Powered PPR Fusion Welder for 20-32mm
View Specifications